
 EN
Air escape and liquid flow
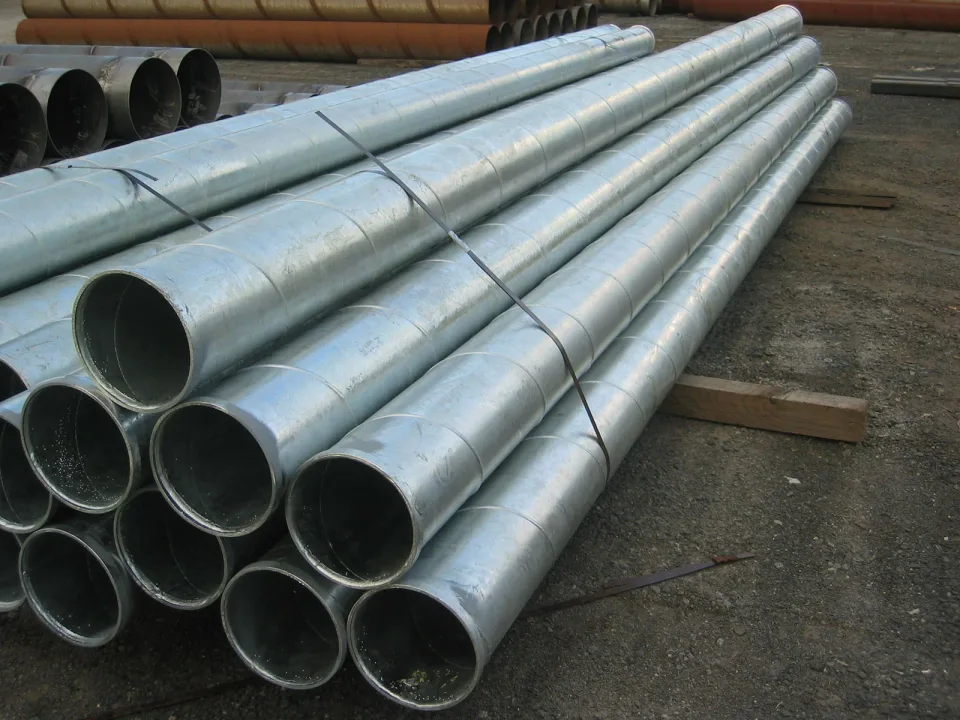
During dip galvanizing, preparation liquids and zinc must be able to enter and leave the component. Enclosed volumes and pockets retaining liquid affect that flow. Venting and drainage openings are therefore more than a cosmetic detail. Internal voids need to be visible in drawings so the galvanizing plant can assess the design.
Why are opening dimensions project-specific?
Section geometry, component length, joint arrangement and dipping orientation influence the openings required. Applying one dimension found online to every component is inappropriate. Internally vented joints may not be visible externally and should be identified in drawings and at acceptance. Missing openings must be resolved with the technical team before processing.
Coordination between fabricator and galvanizer
Track agreed openings against the drawing revision. After fabrication, check that welding or added parts have not blocked passages. Report design changes before shipment. This article is not an opening-sizing instruction: the designer and galvanizing plant must determine details for the component. Proper coordination supports both process safety and coating access.
Describing internal spaces that are not visible
An external elevation may not reveal every void within a welded assembly. Section views and detail drawings make internal passages easier to assess. Seeing an external hole is insufficient if it is unclear which volume the opening serves. Reference the relevant drawings in the component schedule. After fabrication, check that the actual component matches those drawings. Report uncertain enclosed volumes before shipment; a detail requiring component-specific assessment should not be resolved using generic online advice.